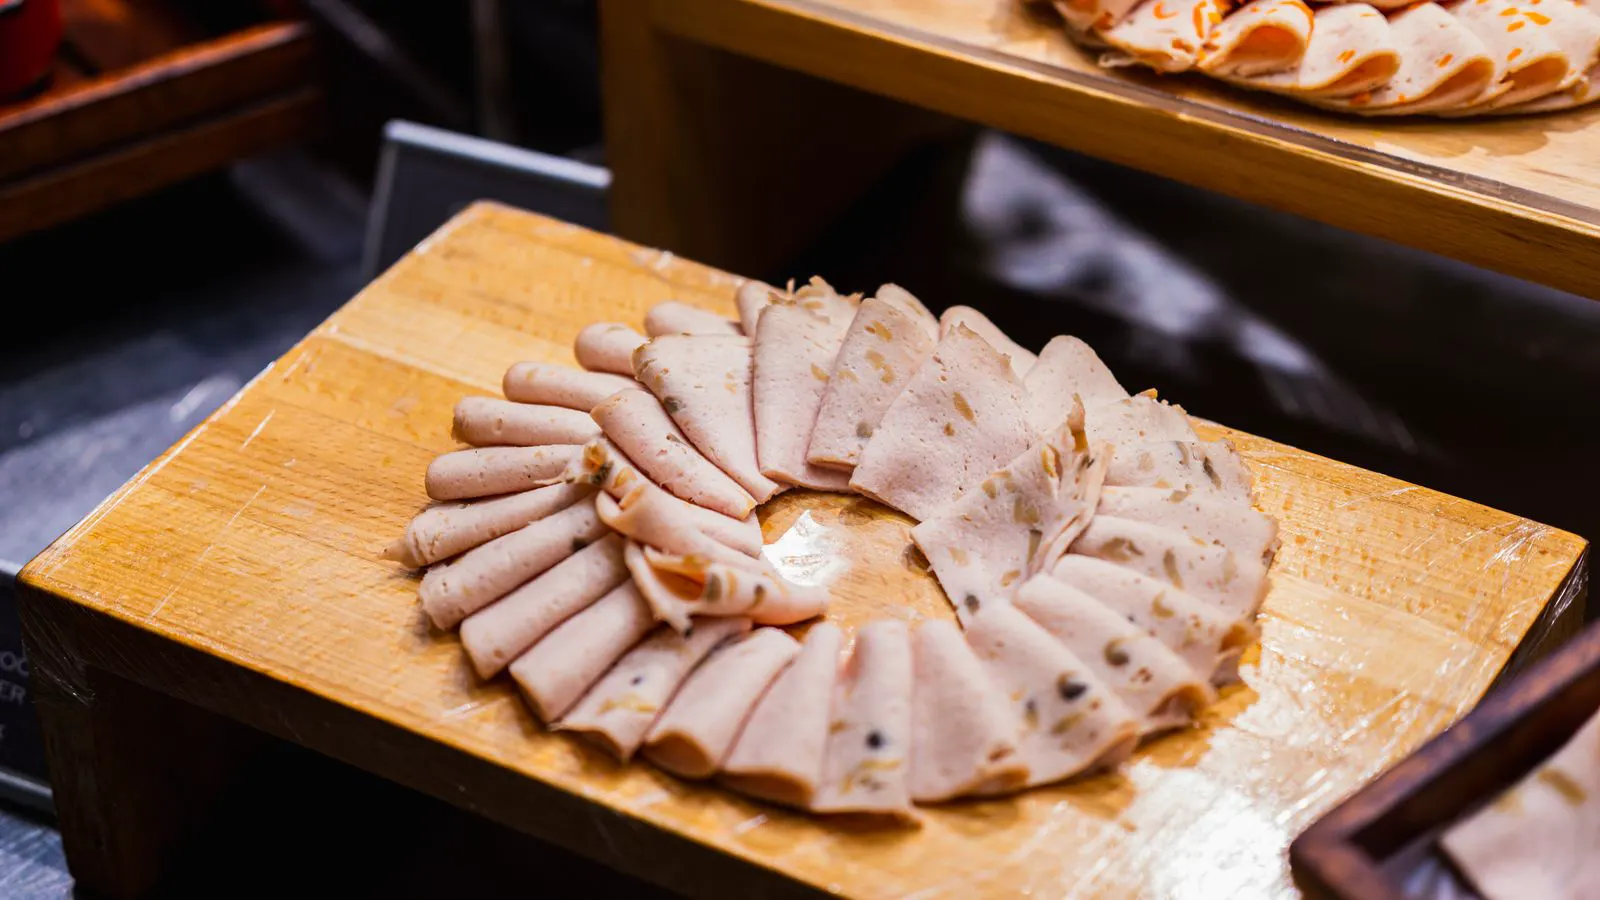
Reduce product debris by aligning blades, controlling feed rates, and maintaining proper guard tension. These steps cut slicing waste and improve hygiene in your processing facility.
- Product debris often comes from uneven blade contact, not just dull edges.
- Adjusting feed speed and guard pressure can significantly reduce trim losses.
- A consistent cleaning and inspection routine prevents debris buildup from becoming contamination.
- Measuring waste before and after adjustments gives a clear baseline for improvement.
- Small mechanical changes usually deliver better results than increasing blade sharpness alone.
Why product debris builds up on slicing lines
Product debris appears when the blade does not cut cleanly through the entire product in one pass. The result is uneven thickness, torn edges, and loose fragments that fall onto the conveyor or into the chute. In most facilities, the debris is not random. It follows a pattern tied to machine setup, product condition, or operator technique.
Before changing anything, identify where the debris lands. If it gathers near the blade guard, the issue may be guard pressure or product positioning. If it falls behind the slicer, the blade may be misaligned or the carriage may be moving too fast. If the debris is fine and powdery, the product may be too soft or the blade may be dull.
This guide walks through a step-by-step approach to reduce product debris, lower slicing waste, and keep the line hygienic.
Prerequisites: What you need before you start
Before adjusting the line, prepare the following:
- A calibrated thickness gauge or digital measuring tool
- A clean, flat work surface for testing
- A spare blade or a sharpening schedule already in place
- A waste bin or container to measure output
- A log sheet to record settings and results
- Access to the machine manual for guard and carriage adjustments
- A small sample of the product you typically slice
Having these items ready prevents guesswork. You will be able to compare settings side by side and track what actually changes the debris level.
Step 1: Baseline your current waste
Measure the product before and after slicing. Weigh a known quantity, slice it, and collect all trim and loose pieces. Record the weight of the finished slices and the weight of the debris. This gives you a baseline.
Without a baseline, you cannot tell whether a change helped or hurt. If you adjust one setting and the waste goes down, you may think it is the blade. But the real cause might have been the feed rate.
Repeat the measurement three times in a row. Average the results. This removes the effect of one odd batch or one operator variation.
Step 2: Check blade alignment
Open the guard and inspect the blade edge. Run your finger lightly along the edge from one end to the other, using proper safety technique. Look for gaps, nicks, or uneven wear. A blade that sits too high on one side will cut deeper on that side and leave thicker, uneven strips.
If the blade is misaligned, correct it according to the machine manual. Many slicers have a leveling screw or a guide rail adjustment. Tighten the bolts securely after adjustment.
A misaligned blade creates product debris because the cut does not separate cleanly. The product tears instead of slicing, and fragments scatter. This is one of the most common causes of waste on a line.
Step 3: Adjust guard pressure
The guard, also called the plunger or pressure bar, holds the product against the blade. If it is too loose, the product shifts during the cut. If it is too tight, it compresses the product and squeezes material out from the edges.
Set the guard pressure so the product stays firm but not deformed. A good test is to place a slice on the carriage and watch how the guard moves. It should press evenly. There should be no visible bending of the product surface.
Incorrect guard pressure is a frequent source of slicing waste. A loose guard causes the product to slide, and the blade cuts at an angle. A tight guard pushes soft products outward, creating thin strips that break off.
Step 4: Control feed speed
Feed speed is the rate at which the operator pushes the carriage toward the blade. If the operator pushes too fast, the blade cannot separate the product cleanly. The result is torn edges and loose fragments.
Reduce the feed speed by a small amount. Test with the same product and the same blade. Collect the debris and compare it to your baseline. If the waste drops, keep the slower speed. If the waste stays the same or increases, the issue is not speed.
A slower feed gives the blade more time to cut through the full thickness. This is especially true for dense or firm products. For soft products, a slower feed can sometimes increase squishing. Find the balance.
Step 5: Match blade sharpness to the product
A dull blade does not just create rough cuts. It increases the force needed to push the product through, which can shift the product under the guard. That shift creates uneven thickness and debris.
Sharpen the blade only when needed. Over-sharpening can remove too much material and change the blade geometry. Under-sharpening leaves a rough edge that tears the product.
For firm products, a sharp edge with a fine grind usually works best. For soft or sticky products, a slightly more aggressive edge can help the blade release the product without pulling. Test both settings and measure the waste.
Step 6: Optimize product presentation
How the product sits on the carriage matters more than most operators expect. If the product is uneven, the blade will cut thicker on one side and thinner on the other. The uneven parts break off as debris.
Prep the product before it reaches the slicer. Remove large lumps, dry the surface if it is too wet, and place the product flat and centered. For irregular shapes, trim the corners slightly so the guard can press evenly.
A consistent product shape reduces slicing waste. It also makes the cut cleaner and keeps the blade from catching on protruding edges.
Step 7: Tune thickness settings
If the target thickness is set too thin, the product has less structural integrity to hold together. The blade cuts, but the slice bends or breaks. The broken pieces become product debris.
Increase the target thickness by a small amount and test. If the waste drops, the original setting was too aggressive. If the waste stays the same, the thickness is not the main issue.
For many products, a slightly thicker slice that is consistent beats a thinner slice that breaks. This is a trade-off. Choose based on the end-use requirement.
Step 8: Verify with a controlled test
After all adjustments, run a controlled test. Use the same product, the same blade, the same operator, and the same settings. Slice a fixed quantity, say five kilograms or a fixed number of pieces. Weigh the finished product and weigh all debris.
Compare the result to your baseline. If the debris weight has dropped, you have a measurable improvement. If not, return to Step 2 and recheck alignment.
Do not change multiple settings at once during the verification step. Change one setting, test, record, and move on. This is how you isolate the cause.
Common mistakes that increase product debris
| Mistake | Effect on Debris | Fix |
|---|---|---|
| Guard pressure too loose | Product shifts, uneven cut | Tighten guard to firm, even contact |
| Guard pressure too tight | Product compresses, edges squeeze out | Loosen guard to reduce deformation |
| Feed speed too fast | Blade tears product | Slow carriage push |
| Blade misaligned | Uneven thickness, torn strips | Level blade per manual |
| Blade dull | High force, product shifts | Sharpen or replace blade |
| Product uneven on carriage | Blade catches, slices break | Prep product, center on carriage |
These mistakes are easy to miss because each one produces a small amount of waste. Together, they add up to a significant loss over a full production run.
Final verification and documentation
Once you have a setting that reduces product debris, document it. Record the guard pressure, feed speed, blade condition, product prep method, and thickness setting. Store the document where the next shift can find it.
Run the line for a full shift before calling the process stable. Debris levels can change as the blade wears or the product temperature shifts. Recheck the waste at the end of the shift.
If the debris returns to baseline, identify what changed. Was the blade used longer? Did the product arrive softer? Adjust accordingly.
A hygienic cutting process is not just about a clean blade. It is about a consistent setup that prevents debris from forming in the first place. The less debris you create, the less you need to clean, and the lower your risk of cross-contamination.
Frequently asked questions
How much product debris is considered normal on a slicing line?
There is no fixed number. It depends on the product, blade condition, and machine type. The goal is to keep it low and consistent. If the weight changes from shift to shift, investigate the cause.
Can a sharper blade always reduce debris?
No. A sharper blade helps, but if the guard pressure, feed speed, or product presentation is off, a sharp blade will still create uneven cuts. Fix the setup first, then sharpen as needed.
What is the safest way to check blade alignment?
Turn off the machine and lock it out. Use the manual to identify the adjustment points. Do not touch the blade edge with a bare hand. Use a guide or a soft tool to feel for gaps.
Should I increase thickness to reduce waste?
Only if the end-use allows it. A thicker slice may reduce breakage, but it changes the product. Test the waste reduction against the product specification before making a permanent change.
How often should I recheck the debris weight?
At least once per shift and after any blade replacement or major setup change. If the product type or temperature changes, recheck more often.