Proper blade maintenance keeps slicers accurate and safe. This guide covers prerequisites, step by step sharpening, and verification methods. Follow these safety procedures to prevent injury and extend tool life.
- Inspect the blade for nicks and wear before starting any sharpening task.
- Lock out and tag the machine to ensure zero energy state before working.
- Use the correct grit sequence for a smooth, durable cutting edge.
- Verify the final edge with a visual check and a soft test cut.
- Document maintenance intervals to track wear and predict replacement needs.
Why Blade Maintenance Matters for Slicing Accuracy
A dull blade pulls material instead of cutting it. This increases force, creates uneven slices, and generates heat that can affect food quality. For operators, the risk of a slip or a kickback rises as the edge becomes uneven. Regular blade maintenance prevents these issues before they stop a production line.
The condition of the edge depends on the product being sliced. Delicate items like cheese or fruit require a finer edge than dense meat or frozen products. Even a small nick in the bevel can cause the blade to skip. This leads to inconsistent thickness and increased wear on the drive mechanism.
Prerequisites Before Starting Knife Sharpening
Prepare the work area and the machine before touching the blade. The operator needs access to the correct sharpening tools, a clean workspace, and a full set of Personal Protective Equipment.
- Lock out the power supply. Remove the key and apply a lockout tag to the main disconnect. This prevents accidental startup during maintenance.
- Wait for the blade to stop moving completely. Verify that the motor has cooled down. Heat can warp the metal or cause burns.
- Remove the blade from the machine. Place it on a padded surface to protect the edge from accidental contact.
- Clean the blade with a food grade cleaner. Remove fat and protein residue. A dirty surface hides nicks and makes grinding inconsistent.
- Gather the sharpening tools. Use a wheel or stone matching the blade geometry. Keep a soft cloth and a clean container for grinding slurry.
These steps ensure a stable and safe environment. Skipping the lockout procedure is the most common cause of serious injury during this task.
Step by Step Knife Sharpening Procedure
Follow this sequence to restore the cutting edge. The goal is to remove a thin layer of metal from the dull areas and create a uniform bevel. Do not try to remove a large amount of material at once.
- Check the bevel angle. Measure the existing angle if a gauge is available. Most slicer blades use a shallow angle, often between 5 and 8 degrees. Match this angle with the sharpening tool. If the angle is wrong, the edge will wear quickly.
- Mark the dull spots. Use a marker on the bevel face. This helps identify the areas that need the most metal removal. The marker also fades as you grind, giving visual feedback on progress.
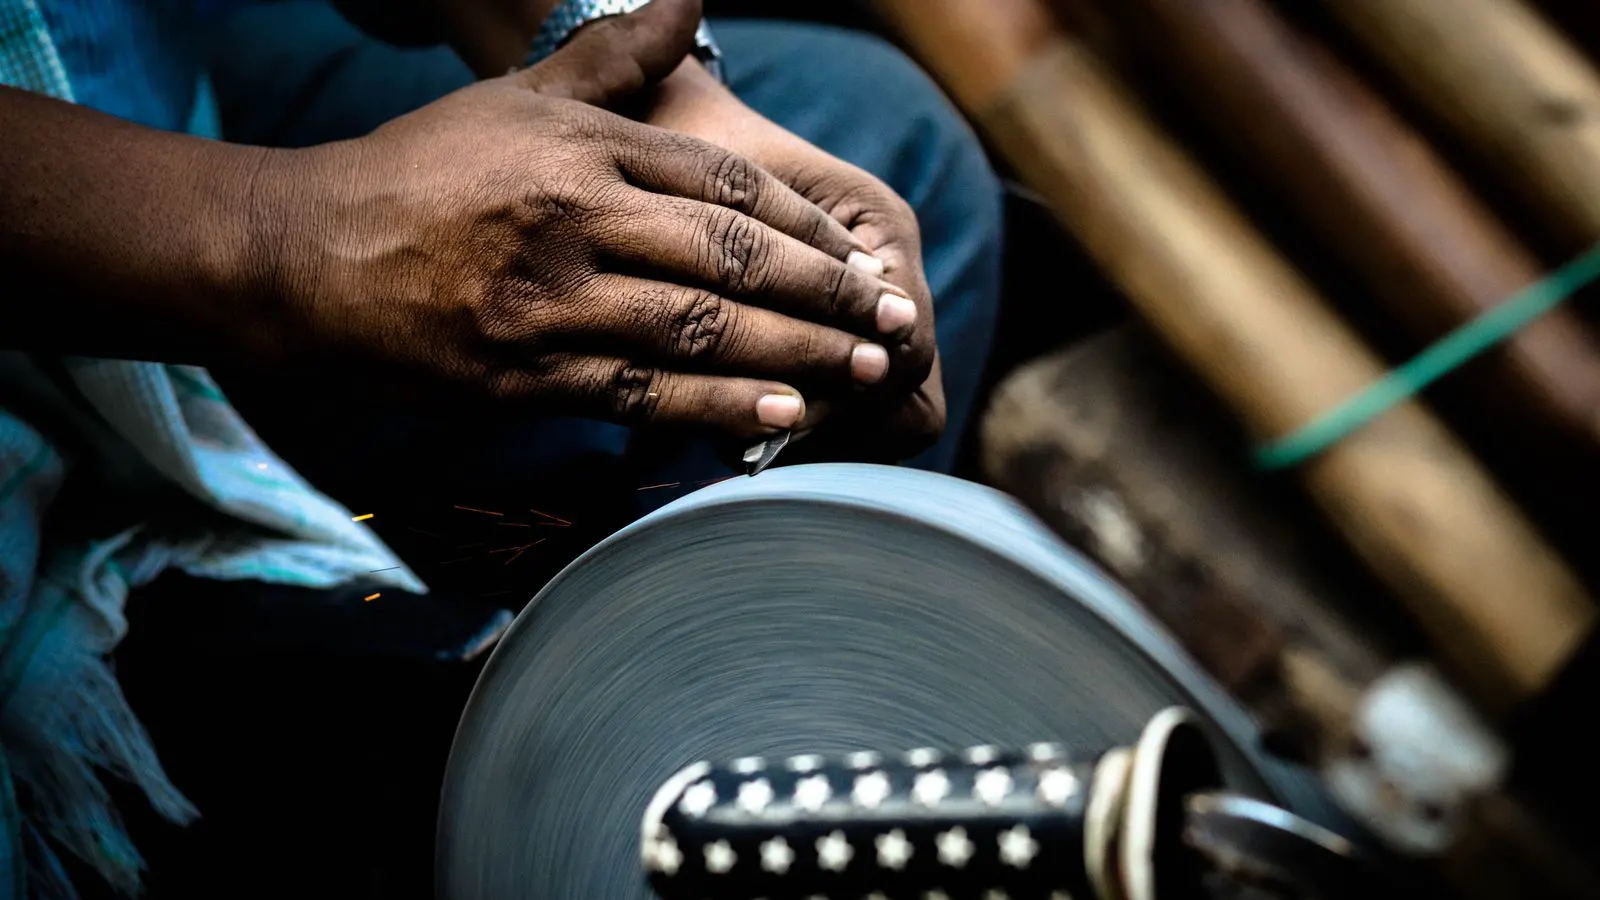
- Start with a coarse pass. Use a medium grit wheel or stone. Make light, even strokes along the bevel. Keep the blade moving to avoid overheating the metal. Overheating can change the temper of the steel, causing the edge to chip.
- Remove the marker. Check the surface frequently. When the marker is gone, the metal has been removed evenly. If the marker remains in the center, the edge is still high there.
- Transition to a fine grit. Switch to a finer stone or wheel. This refines the microscopic edge that was created in the previous step. The fine pass removes the burr and smooths the transition to the flat face.
- Hone the flat face. Gently rub the flat side of the blade against a fine honing stone. This aligns the microscopic teeth and removes any remaining burr from the bevel. Do not press hard on this step.
- Clean the final edge. Wipe the blade with a clean, dry cloth. Check the edge under bright light. It should reflect light evenly without dark patches or visible scratches.
This process restores the geometry of the edge. The result is a blade that cuts with less resistance and less heat generation.
Common Mistakes That Ruin Blade Maintenance
Even with the right tools, bad technique can ruin a blade. These errors are frequent in high volume environments where operators rush the task.
| Mistake | Consequence |
|---|---|
| Overheating the steel | Changes temper, causes edge to chip or roll |
| Uneven pressure | Creates a curved bevel, leads to vibration |
| Skipping the fine pass | Leaves a burr, causes tearing instead of cutting |
| Using wrong grit | Removes too much metal or does not refine edge |
| Ignoring the flat face | Leaves burr on the back, dulls the cutting side |
Overheating is the most damaging error. The steel in a slicer blade is hardened to a specific level. If the temperature rises too high during grinding, the hardness drops. The edge loses its ability to hold a sharp shape. This forces the next maintenance cycle to remove even more metal.
Uneven pressure creates a curved edge. The blade may look straight but will vibrate during operation. This vibration transfers stress to the bearings and the motor. It also makes the slices uneven. Always keep the weight of the blade and the tool constant across the entire bevel.
Safety Procedures for Blade Work
Safety is not optional. A sharp blade is a dangerous object if handled without care. The operator must maintain a defensive posture and keep hands clear of the cutting path.
- Wear cut resistant gloves. Use gloves rated for sharp objects. These protect the fingers during handling and when placing the blade on the tool.
- Support the blade fully. Never hold the blade by the edge. Use a blade holder or a padded clamp. This prevents the blade from slipping and cutting the operator.
- Keep the work area clear. Remove loose clothing, jewelry, and tools that are not part of the sharpening process. Long hair must be tied back.
- Inspect for cracks. Look for small cracks near the mounting holes or the center hub. A cracked blade can shatter during sharpening or operation.
- Dispose of waste properly. Grinding slurry and metal dust can be slippery or sharp. Use a dedicated container for disposal.
These precautions protect the operator and the surrounding team. A single slip can cause a severe laceration that requires medical attention.
Final Verification and Testing
Do not reinstall the blade until it passes a final check. The goal is to confirm that the edge is sharp, even, and free of burrs. This step ensures that the blade will perform correctly in the production environment.
- Visual inspection. Hold the blade up to a bright light. Look for uniformity in the bevel. Check the flat face for any dark spots or burrs.
- Feel for the burr. Using the back of a finger, very gently feel the edge. There should be no sharp protrusion or burr. If a burr is present, repeat the fine pass.
- Perform a test cut. Install the blade in the slicer. Run it at low speed with a block of soft material, such as a potato or a block of cheese. The blade should slice through with minimal force.
- Check slice thickness. Measure the slices with a caliper. They should be consistent within the machine’s tolerance. Variation indicates an uneven edge or a misaligned blade.
- Listen for noise. Run the slicer for a few minutes. Listen for grinding or vibration sounds. A sharp blade runs smoothly.
If the test cut is difficult or the slices are uneven, the blade needs more work. Do not force the material. A dull blade will pull and cause the operator to lean on the carriage, which is unsafe.
Maintenance Scheduling and Documentation
Track the condition of the blade over time. Keep a log of each sharpening session. Note the date, the operator, the tools used, and the observed condition of the edge.
Regular sharpening extends the life of the blade. A blade that is sharpened before it becomes dull requires less metal removal each time. This preserves the overall geometry of the tool. If a blade is only sharpened after it is very dull, the operator may remove too much metal, shortening the blade’s usable life.
Review the log periodically. If the intervals between sharpenings are getting shorter, the blade may be worn out. It might be time to replace it. This planning helps avoid sudden downtime during a production run.
Frequently asked questions
How often should I sharpen a food slicer blade?
Sharpen the blade when the edge begins to pull or when slices become uneven. For high volume use, check the blade every few days. For light use, weekly checks are usually sufficient.
Can I use a standard kitchen knife sharpener on a slicer blade?
No. Kitchen sharpeners are not designed for the size and geometry of a slicer blade. Use a dedicated tool that matches the blade angle and bevel width.
What is the best way to clean the blade after sharpening?
Wipe the blade with a clean, dry cloth to remove any metal dust. Use a food grade cleaner if any residue remains. Ensure the blade is completely dry before installation.
How do I know if the blade is overheated during sharpening?
Touch the bevel face with the back of your hand after a short pass. If it feels too hot to hold comfortably, you are working too fast or with too much pressure. Allow it to cool.
Can I sharpen a blade if it has a chip?
Yes, you can remove a small chip with a coarse grit stone. If the chip is large or the edge is severely damaged, consider replacing the blade.