Canning seal failure usually stems from improper lid placement, insufficient heat, or worn sealing heads. This guide lists symptoms, causes, and fixes in a table, then outlines prevention steps for stable production.
- Check lid centering and sealing head condition before blaming the heat process.
- Log seal strength and visual defects to spot trends before a full batch fails.
- Keep sealing parameters aligned with the specific can and lid material used.
- Train operators to distinguish between a mechanical seal fault and a process timing error.
A weak seal on a can is not just a cosmetic issue. It is a direct signal that the packaging line is not delivering the vacuum or heat integrity required for shelf stability. When canning seal failure appears, the root cause is rarely the steam sterilization stage. It is almost always located in the sealing equipment or the immediate handling steps before and after the can enters the sterilizer.
This guide breaks down the most common failure modes. It separates mechanical issues from process errors so you can isolate the problem quickly. The table below maps symptoms to likely causes and corrective actions. Use it as a first-pass diagnostic tool when the lab reports poor seal strength or the inspection team rejects cans for leakage.
Identify the physical symptom first
Before adjusting machine settings, walk the line and inspect the rejects. A can with a dented lid is a different problem than a can with a flat, uncrushed lid. The shape of the lid tells you whether the seal head applied even pressure or if the can was misaligned during the sealing cycle.
Look for three specific visual cues:
- Lid centering. If the lid sits off-center, the sealing jaw or the infeed conveyor is likely misaligned. The vacuum chamber may have pulled the lid slightly during the initial fill.
- Seal ring deformation. A proper seal crushes the ring into a uniform bead. If the bead is thin or broken in spots, the sealing head may be worn or the pressure setting is too low.
- Lid discoloration. Dark spots on the lid edge can indicate excessive heat or a chemical reaction with the filling. This points to a process temperature issue rather than a mechanical one.
Diagnose mechanical faults in the sealing equipment
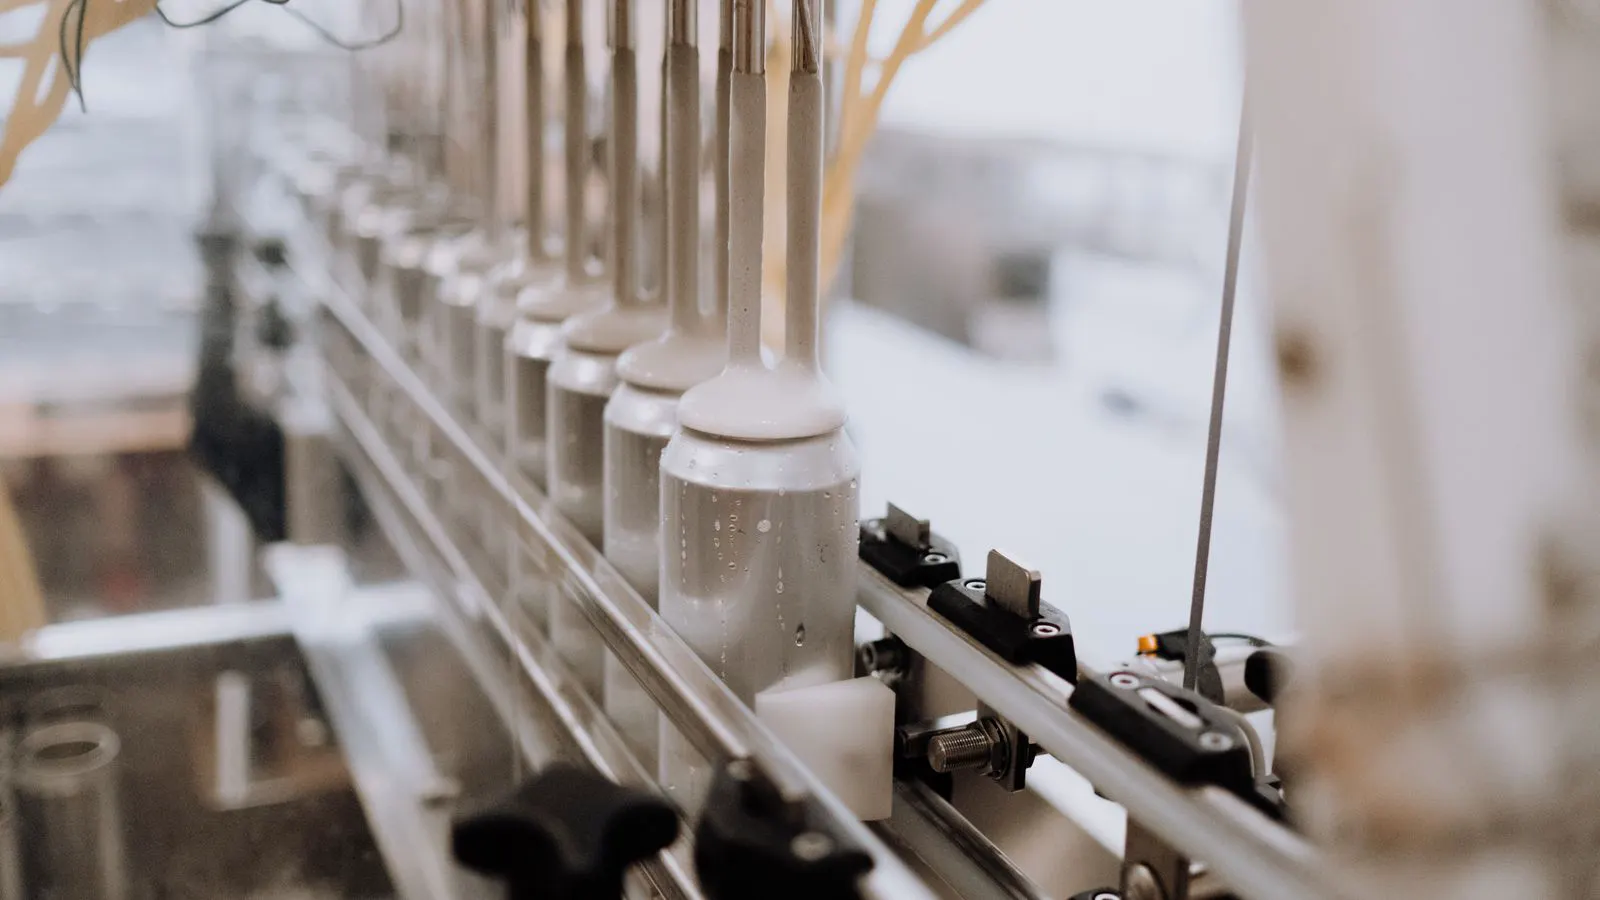
Mechanical failures are the most common source of inconsistent seal integrity. The sealing head is the critical component, but the seals, gaskets, and alignment guides matter just as much. Over time, the rubber or polymer seals inside the sealing head degrade. They become hard, crack, or flatten. This reduces the vacuum pressure needed to draw the lid into the seal zone.
Check the sealing head assembly during your scheduled maintenance. Look for nicks in the sealing surface. Even a small scratch can prevent the lid ring from crushing evenly. Replace seals before they reach the end of their service life. Do not wait for a visible crack. A slightly compressed seal will leak slowly and cause intermittent failures that are hard to trace.
Alignment is the second mechanical culprit. The can must sit perfectly centered under the sealing head. If the infeed conveyor is worn or the guide rails are loose, the can can shift by a few millimeters. That shift is enough to prevent the sealing jaw from engaging the lid ring properly. Use a feeler gauge to check the gap between the can rim and the guide rails. Adjust the tension on the conveyor chain to remove slack. A loose chain causes the can to bounce slightly during the sealing cycle, which interrupts the vacuum pulse.
Check the process timing and vacuum parameters
If the mechanical parts look good, the problem is likely in the process parameters. The sealing process involves a specific sequence: fill, vent, seal, and cool. If the venting step is too short, steam remains trapped between the lid and the can. When the vacuum is applied, the steam condenses and creates a false vacuum. The lid may look sealed, but the internal pressure is not low enough for long-term stability.
Review your process sheet for the current product. Different fill volumes require different venting times. A heavier, denser product needs a longer vent to release trapped air. If you changed the product formulation or the fill weight, the sealing parameters must be updated. The vacuum pressure must be sufficient to crush the lid ring. If the pressure is too low, the ring stays flat. If it is too high, it may crack the lid or deform the can body.
The cooling phase is often ignored. After the seal is made, the can must cool to a specific temperature before it leaves the sealing station. If the can is too hot, the lid can expand and break the seal. If it is too cold, the vacuum may collapse before the lid fully sets. Monitor the outlet temperature of the sealing station. It should be consistent across all cans. A fluctuating temperature suggests a problem with the cooling water flow or the steam trap in the cooling jacket.
Verify the lid and can material quality
Even a perfectly tuned machine will produce seal failures if the raw materials are substandard. The lid ring is the most critical part of the packaging. It is a thin band of metal that must deform plastically to create the seal. If the steel or aluminum grade is wrong, the ring may not crush properly. It may spring back or crack.
Check the supplier certificates for the lid material. The tensile strength and ductility must match the sealing equipment’s requirements. A brittle lid ring will shatter during the sealing cycle. This creates a hole in the lid and an immediate leak. A soft lid ring may not hold its shape. It will flatten under low vacuum pressure, resulting in a weak seal that fails during storage.
The can body also matters. If the can rim is not flat, the lid cannot sit evenly. This can happen if the canning machine’s forming station is worn. The rim must be uniform to ensure the lid ring makes contact at all points around the circumference. Inspect a sample of cans from the forming station. Use a ruler to check the flatness of the rim. If the rim is bent or uneven, the canning machine’s forming die needs adjustment or replacement.
Implement a preventive maintenance schedule
Fixing seal failures reactively is expensive. It stops the line and creates waste. A preventive maintenance schedule stops most seal failures before they start. The sealing equipment should be inspected weekly. This includes checking the alignment of the sealing head, the condition of the seals, and the tension of the conveyor.
Monthly, you should perform a deeper inspection. Clean the sealing surface with a soft cloth and a mild solvent. Remove any residue from the canning process. Check the vacuum pump. A vacuum pump with a worn impeller or a leaking gasket will not hold the required pressure. The pressure gauge may read correctly, but the pump may be struggling to maintain it under load. Test the pump by running it for a fixed time and measuring the pressure drop. If the drop is higher than your baseline, the pump needs service.
Quarterly, recalibrate the process controls. The temperature sensors and pressure transducers drift over time. Calibration ensures that the machine is actually applying the correct heat and vacuum. Use a certified reference instrument to check the readings. If the machine says 100 degrees but the reference shows 105 degrees, the control loop is wrong. Correcting this prevents over-processing or under-processing of the can.
Document every failure and trend
Keep a log of every seal failure. Record the date, the machine ID, the product, and the specific symptom. Note the operator and the shift. This data reveals patterns. If failures only happen at the start of a shift, the problem may be in the warm-up procedure. If they only happen on a specific product, the process parameters for that product are wrong. If they happen randomly, it is likely a mechanical issue like a worn seal or a loose guide.
Review the log monthly with your maintenance and quality teams. Look for trends. A small increase in seal failures is a warning sign. It may be the first stage of a major mechanical failure. Addressing it early prevents a batch of failed cans from reaching the warehouse.
Prevention tips for stable seal integrity
Prevention is simpler than troubleshooting. These daily and weekly habits keep the sealing equipment in good shape.
- Check lid placement every hour. Visually inspect the first three cans of every shift. If the lid is off-center, stop the line and check the infeed.
- Monitor vacuum pressure continuously. Set up an alarm if the pressure drops below the set point. A manual check is not enough. The machine must detect the drop in real time.
- Replace seals on a schedule. Do not wait for a failure. Replace the sealing head seals every three to six months, or more often if you run heavy products.
- Keep the sealing surface clean. Residue from the filling can build up on the sealing jaw. It prevents the lid ring from crushing evenly. Clean it after every changeover.
- Train operators on the symptoms. Operators are the first to see a defect. Teach them to recognize a broken seal bead, a dented lid, or an off-center lid. Encourage them to report these issues immediately.
Seal integrity is the foundation of shelf stability. When canning seal failure appears, it is a signal to check the mechanical, process, and material factors in order. Start with the physical inspection. Then check the machine parameters. Finally, verify the raw materials. A systematic approach will save time and reduce waste.
Frequently asked questions
Can a canning machine fix a weak seal without changing the process?
Sometimes. If the seal is weak due to low vacuum pressure, adjusting the pump or replacing a worn seal can fix it. If the seal is weak due to incorrect heat, changing the process is required.
What is the first thing to check when a can leaks from the seal?
Check the lid centering and the shape of the seal bead. If the lid is off-center, the problem is mechanical alignment. If the bead is broken, the problem is likely vacuum pressure or lid material quality.
How often should I inspect the sealing head seals?
Inspect them weekly for visible damage. Replace them every three to six months as part of preventive maintenance. Replace them sooner if you run high-volume or high-heat products.
Does the type of filling affect seal integrity?
Yes. Acidic or viscous fillings can build up residue on the sealing surface. This can prevent the lid from seating properly. Clean the sealing surface after every changeover to different products.
Is a seal failure always a machine problem?
No. Seal failure can be caused by poor lid material, incorrect process timing, or operator error. Always check the materials and process parameters before blaming the machine.