This checklist helps engineers verify retort pressure gauges for accuracy, safety, and documentation before purchase. It covers calibration, materials, and pre-purchase checks to prevent costly errors and ensure reliable process control.
- Verify gauge calibration against traceable standards before accepting delivery.
- Check gauge body materials for corrosion resistance in high-humidity environments.
- Ensure pressure gauge documentation includes calibration certificates and material specs.
- Confirm gauge type and range match your specific retort process requirements.
- Test alarm and shutdown interlocks to prevent overpressure incidents.
Why Pressure Gauges Matter for Retort Safety
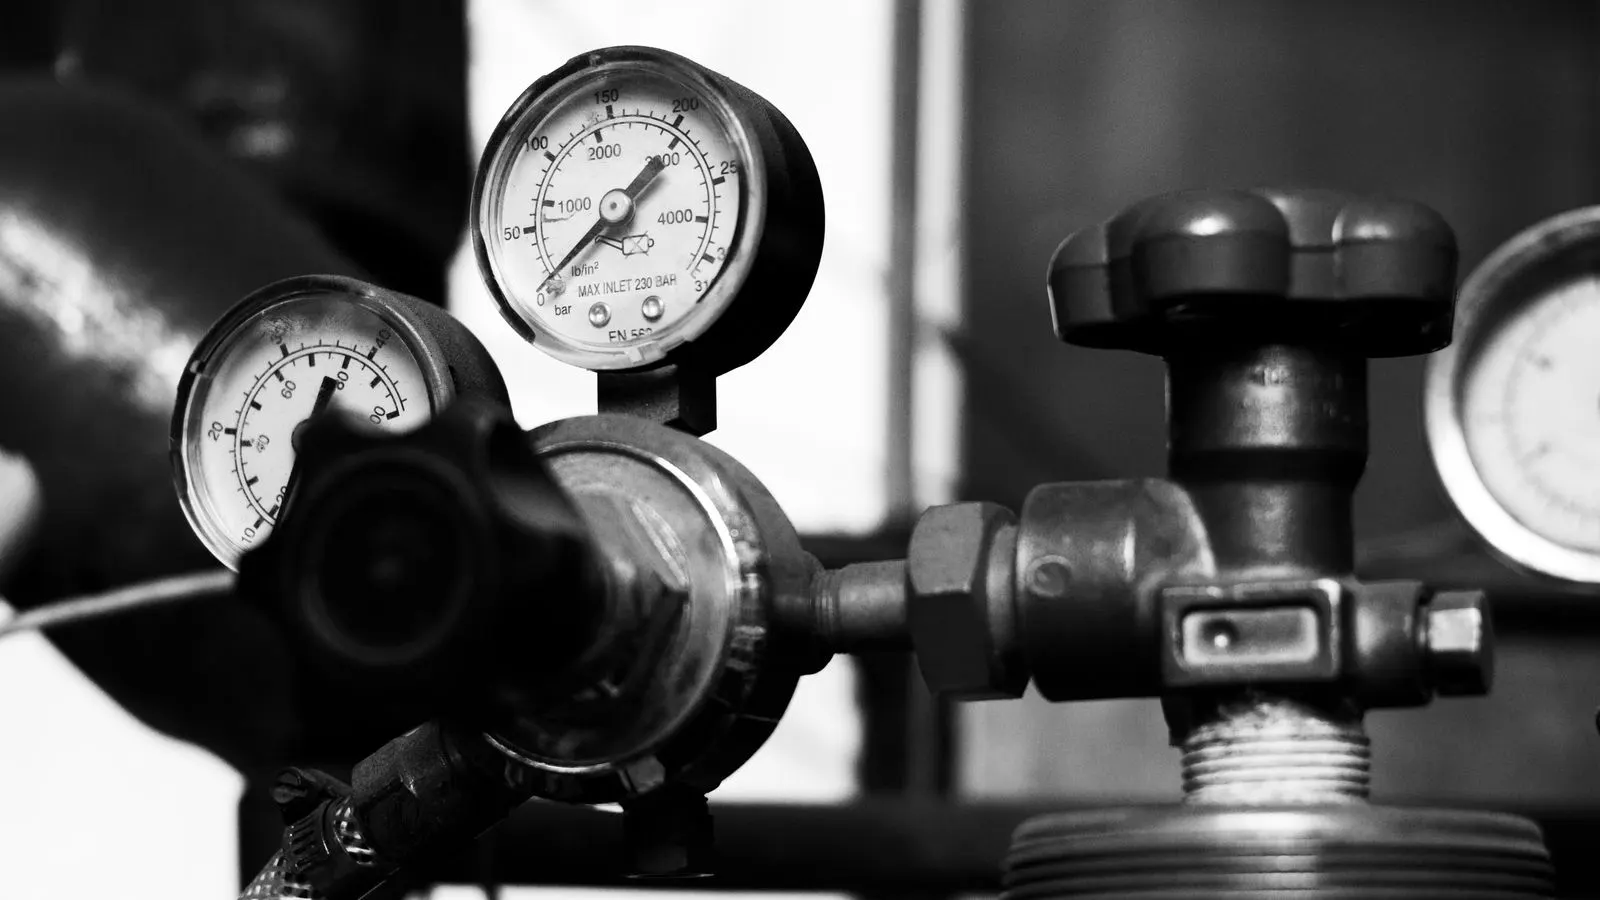
Retort pressure gauges are the primary safety and process control instruments in canned food processing. They monitor steam pressure inside the retort chamber, which directly controls the sterilization temperature and product safety. A gauge that reads incorrectly can lead to under-sterilization or over-processing, both of which have serious consequences.
This checklist is for engineers and procurement teams who are in the pre-purchase phase. It focuses on the verification steps you should complete before finalizing an order for new retorts or replacement gauge assemblies. The goal is to catch accuracy, material, and documentation issues early, when they are cheap to fix.
Confirming Gauge Accuracy and Calibration
Accuracy is the first point of verification. A pressure gauge that drifts over time can compromise your entire sterilization cycle. Before accepting delivery, verify the following:
- Ask the supplier for a current calibration certificate. The certificate should state the calibration date, the reference standard used, and the uncertainty range.
- Request a traceability chain. The calibration should be traceable to a recognized national standard. Ask which standard was used.
- Check the gauge range. The gauge should be sized so your operating pressure falls between 25 and 75 percent of its full scale. A gauge with a range that is too wide for your process will give poor reading accuracy at low pressures.
- Verify the dial type. For retorts, a direct-read analog gauge is common, but digital transmitters are increasingly used. If using digital, confirm the output signal type, such as 4-20 milliamp or 0-10 volt, matches your control system.
A common mistake is accepting a gauge based on a generic spec sheet. Always request the specific calibration report for the exact unit being shipped. If the supplier cannot provide it, treat that as a red flag.
Verifying Materials and Construction
Retort environments are wet and hot. The gauge body and its mounting hardware must withstand repeated steam cycles and occasional cleaning.
Check these material points:
- Body material: Brass is common for low-cost gauges, but stainless steel is preferred in high-humidity or aggressive cleaning environments. Stainless steel resists corrosion better over time.
- Case finish: A polished or passivated stainless finish is easier to clean and less likely to harbor bacteria. Avoid painted cases in wet areas.
- Connection type: Verify the connection thread matches your retort manifold. Common sizes are 1/2 inch and 3/4 inch NPT. A thread mismatch will require adapters, which add failure points and leak risks.
- Seal type: If the gauge uses an O-ring or gasket, confirm the material is compatible with steam and any cleaning chemicals you use.
A gauge with a cracked or corroded body is a safety risk. Inspect each unit visually before signing the delivery note.
Matching Gauge Type to Process Requirements
Not all retort processes are the same. The type of gauge you need depends on your specific sterilization method.
| Process Type | Typical Pressure Range | Recommended Gauge Type |
|---|---|---|
| Low-acid canned goods | 120 to 150 degrees Celsius | Bourdon tube or digital transmitter |
| High-acid canned goods | 100 to 120 degrees Celsius | Bourdon tube |
| High-speed canning | Variable, often higher pressure | Digital transmitter with fast response |
| Batch retorts | Fixed setpoint per batch | Analog direct-read |
For high-speed continuous retorts, a digital pressure transmitter is often preferred over a simple analog gauge. It can send a live signal to the PLC and trigger automatic shutdown if pressure exceeds a safe limit. For standard batch retorts, a high-quality analog gauge with a clear, durable dial is usually sufficient.
If you are upgrading from an older retort, check whether the existing manifold supports the new gauge type. Sometimes a new gauge requires a different mounting flange or a new pressure relief valve connection.
Reviewing Documentation and Compliance
Documentation is as important as the physical gauge. Without proper records, you cannot prove that your equipment met safety standards at the time of purchase.
Before ordering, confirm you will receive:
- Calibration certificates for each individual gauge.
- Material safety data sheets for the gauge body and seals.
- Installation and maintenance instructions specific to the gauge model.
- Warranty terms. Standard analog gauges often carry a one-year warranty. Digital transmitters may have longer warranties depending on the supplier.
In many jurisdictions, pressure vessels and their safety devices are subject to inspection. Your pressure gauge documentation may be required during a periodic inspection. Keep the calibration certificates in your equipment maintenance file. If a regulator asks for proof of calibration, having the original certificates ready will save time.
A red flag is a supplier who offers a “generic” calibration certificate for all units. Each gauge should have its own individual record.
Testing Alarm and Interlock Function
Many modern retorts use pressure gauges as part of a safety interlock system. The gauge is not just a display; it is a control input. If the pressure rises above a set limit, the interlock should cut off the steam supply.
Before finalizing the order, verify the following:
- Ask how the interlock is designed. Is it a mechanical limit switch on the gauge stem, or an electronic sensor with a PLC logic output?
- Confirm the alarm setpoint. Your alarm should trigger at a pressure below the maximum allowable working pressure of the retort.
- Test the shutdown function. If possible, request a factory test where the gauge is driven to its trip point and the interlock is activated.
- Check response time. A slow-responding gauge may not trigger the shutdown quickly enough during a rapid pressure spike.
A gauge that is only used for visual reading and not connected to any safety interlock is a compliance risk. Always confirm the gauge’s role in the safety system.
Pre-Purchase Inspection and Acceptance
The final step is a physical inspection upon delivery. Do not accept the gauge without checking the items below.
- Unpack each gauge and compare the model number to the purchase order.
- Check the dial for damage. Cracks, blurred markings, or a needle that does not rest at zero are signs of poor quality.
- Inspect the connection thread for burrs or deformation.
- Verify the serial number is legible and matches the calibration certificate.
- Check the packing. Gauges should be protected from impact. A crushed case or a gauge that has been dropped is a risk.
If the supplier ships gauges in a single shared box without individual protective padding, that is a sign of poor handling. Request that the supplier improve packaging if this happens.
Red Flags to Watch For
When reviewing quotes and specs, watch for these warning signs:
- No calibration certificate offered. This suggests the gauges have not been tested against a standard.
- Vague material descriptions. “Metal body” is not specific enough. You need to know if it is brass, carbon steel, or stainless steel.
- No warranty or a very short warranty. A one-month warranty indicates the supplier does not stand behind the product.
- Pressure range that does not match your process. If your retort operates at 130 degrees Celsius, a gauge rated for 0-200 degrees Fahrenheit is too small and will saturate too quickly.
- No documentation on interlock compatibility. If the gauge is supposed to trigger a shutdown, the supplier should explain how it connects to your control system.
If you encounter any of these red flags, stop the purchase process. Ask for clarification in writing. If the supplier cannot provide clear answers, consider a different supplier.
Final Verification Checklist
Copy this checklist for your pre-purchase review. Complete each item before signing the purchase order or accepting delivery.
- Gauge model and serial number match the purchase order.
- Calibration certificate provided for each unit, with traceability stated.
- Gauge range matches process pressure, with operating point between 25 and 75 percent of full scale.
- Body material is stainless steel or confirmed suitable for steam and cleaning chemicals.
- Connection thread matches the retort manifold.
- Gauge type is appropriate for the process, analog or digital.
- Interlock function is confirmed and documented.
- Warranty terms are acceptable.
- Material safety data sheets are available.
- Physical inspection upon delivery is completed without defects.
This checklist is not a substitute for a formal engineering review. It is a practical tool to help you verify the basics before money changes hands. Use it alongside your site’s standard operating procedures for equipment acceptance.
Common Questions
Is a pressure gauge required for every retort?
Yes. Every pressure vessel, including retorts, must have a means to monitor internal pressure. A pressure gauge is the most common and required method. It is a basic safety and regulatory requirement in most food processing facilities.
How often should pressure gauges be recalibrated?
Recalibration frequency depends on your site’s quality management system and local regulations. A common practice is to calibrate annually, or after any incident where the gauge may have been damaged. Always follow your internal procedures and applicable standards.
Can I use a gauge from a different supplier on my existing retort?
Yes, but you must verify compatibility. The new gauge must match the connection thread, the pressure range, and the material requirements. It must also be compatible with any existing interlock system. A gauge from a different supplier is not automatically interchangeable.
What is the difference between a pressure gauge and a pressure transmitter?
A pressure gauge is an instrument that provides a direct visual reading. A pressure transmitter converts pressure into an electrical signal, such as 4-20 milliamp, which can be sent to a control system. Transmitters are used when you need automated control or data logging.
Can I install a digital gauge on an older analog retort?
In many cases, yes. You would need to replace the analog gauge with a digital transmitter and modify the control system to accept the new signal. This requires an engineer to review the electrical and mechanical compatibility. It is not a simple swap.
===END===